

A steel formwork diagram for a precast column mould is not a general arrangement drawing. It is a contract. Every line on it—panel thickness, rib spacing, bolt hole diameter, stripping angle—translates directly into your cycle time, your surface finish, and your scrap rate. If you cannot read those lines, you are buying a black box. This article walks through the diagram from the workshop side, so you can interrogate a supplier before you wire a 30% deposit.
Start with the panel schedule, not the 3D view
The first page of any serious steel formwork diagram is the panel schedule. It lists every plate, its thickness, its material grade, and its edge preparation. For precast work, you will see 3 mm to 6 mm steel panels. The choice is not arbitrary. A 3 mm panel on a 2.4 m high column mould will deflect under a 60 kN/m² pour pressure. A 6 mm panel will not. But a 6 mm panel adds roughly 47 kg per square metre compared to 3 mm, which changes crane and handling requirements.
Ask the supplier to show the deflection calculation. If the diagram shows 4 mm panels with ribs at 300 mm centres, the maximum span between ribs is 300 mm. That is a stiff mould. If ribs are at 500 mm centres, the panel will flex more, and you may see 1.5 mm to 2 mm of bulge on a 3 m pour. For architectural precast, that is scrap. For a drainage culvert, it is acceptable.
Rib spacing and stiffener layout: the real stiffness story
Ribs are not decoration. They are the load path. In our workshop, we fully weld ribs and stiffeners to the panel. A typical column mould diagram shows vertical ribs every 400 mm and horizontal stiffeners every 600 mm. That layout resists a pour rate of 3 m/hr without visible deflection. If you push to 5 m/hr, you need ribs at 300 mm centres or a thicker panel.
Look at the weld symbols. A 6 mm fillet weld on both sides of a rib is standard. A 4 mm intermittent weld is a cost-saving measure that will crack after 20 to 30 reuses. The diagram should specify continuous welds on all primary ribs. If it does not, ask why.
Stripping sequence and draft angle: where cycle time is won or lost
The stripping sequence is drawn as a series of steps. A good diagram shows the order of bolt removal, the use of jacking screws, and the draft angle on the mould faces. For a 4 m high wall panel, a draft angle of 1.5° per side is typical. That is 26 mm of taper over 1 m. Without it, you will need a crane to pull the panel, and you risk edge spalling.
Jacking screws are usually M20 or M24, rated for 15 to 20 tonnes each. The diagram should show their positions at 1 m centres along the mould base. If they are missing, your stripping time will double. In a precast plant running 8 to 12 cycles per day, that is the difference between profit and loss.
Bolt torque and hole tolerances: the details that cause leaks
Every connection in a steel formwork diagram has a bolt size and a torque value. For M16 bolts, the recommended torque is 190 Nm. For M20, it is 370 Nm. Under-torque and the mould will leak grout. Over-torque and you will strip the threads after 10 to 15 cycles.
Hole tolerances matter too. Our panels are drilled to +/-0.5 mm. If the diagram shows +/-1.5 mm, the bolts will bind. You will need a hammer to assemble the mould. That adds 15 to 20 minutes per cycle. Over a 100 cycle project, that is 25 to 33 hours of lost production.
Comparing formwork options: a decision table
Use this table to compare three common configurations for a 3 m high precast column mould. The numbers are typical market ranges for guidance only, not a quotation.
| Configuration | Panel thickness | Rib spacing | Max pour rate | Reuse cycles | Typical market range (USD) |
|---|---|---|---|---|---|
| Light-duty | 3 mm | 500 mm | 2 m/hr | 60–80 | 1,800–2,500 |
| Standard | 4–5 mm | 400 mm | 3 m/hr | 80–100 | 2,800–3,800 |
| Heavy-duty | 6 mm | 300 mm | 5 m/hr | 120+ | 4,200–5,500 |
Do not choose heavy-duty if you are casting 20 columns. The extra 1,400–1,700 USD per mould will not pay back. Choose light-duty only if your pour rate never exceeds 2 m/hr and your surface finish is not architectural. For most precast plants running 50 to 200 cycles per year, standard is the sweet spot.
What the diagram does not tell you: workshop realities
A diagram is a promise. The workshop is where it is kept or broken. Ask these questions before you approve the drawing:
- Jig assembly: Are panels assembled on a jig or freehand? A jig holds +/-0.5 mm tolerance. Freehand holds +/-2 mm.
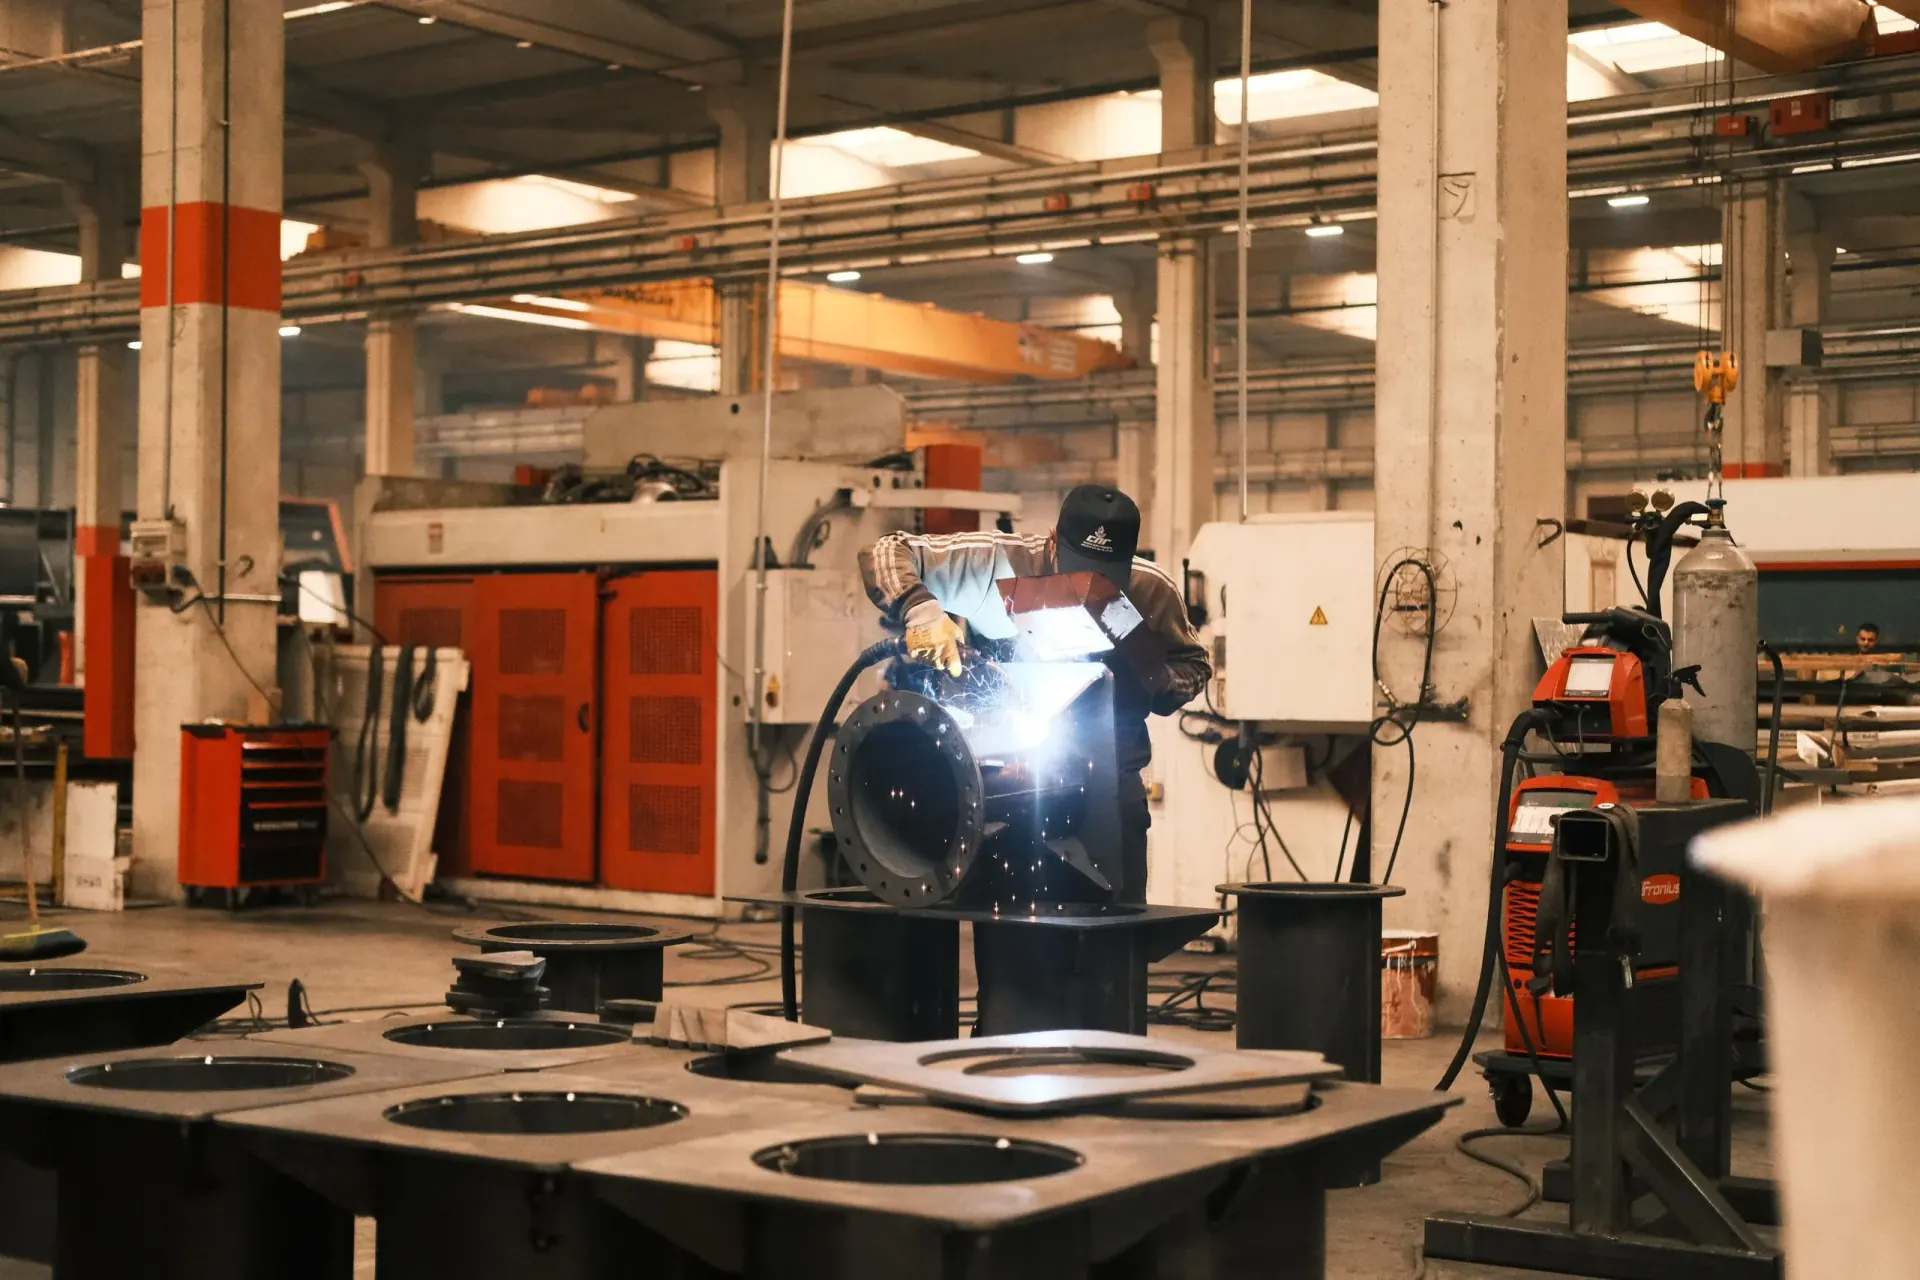
- Welding sequence: Is the welding sequence specified to control distortion? We weld in a balanced sequence, alternating sides, to keep the panel flat.
- Stress relief: For heavy-duty moulds, is stress relief performed after welding? Without it, the mould will move after 30 to 40 cycles.
- Surface preparation: Is the mould face ground and polished? A Ra 3.2 finish gives a smooth concrete surface. A rough finish will transfer to your product.
If the supplier cannot answer these, the diagram is fiction.
Lead time, payment, and documents: the commercial diagram
The commercial terms are part of the selection. For stock moulds, lead time is 7–10 working days. For customised formwork, it is 15–25 working days after deposit. Payment is 30% deposit by T/T, balance against copy of B/L. We ship FOB Tianjin, with CIF or CFR available on request. Documents include CI, PL, MTC, CO, and FORM E. There is no MOQ.
One more number: a 20 ft container holds roughly 12 to 15 tonnes of formwork. A 3 m column mould weighs about 450 kg. So you can fit 25 to 30 moulds in one container. That is your freight arithmetic.
When NOT to choose a steel formwork diagram
Steel formwork is not always the answer. If you are casting 5 columns, timber or plywood formwork will cost less. If your pour rate is under 1 m/hr and your tolerance is +/-5 mm, steel is overkill. If you need a one-off complex shape, 3D-printed formwork may be faster. But for 60+ reuses, steel wins on cost per cycle. The diagram is your tool to verify that the steel you buy will actually deliver those cycles.
Read the diagram like a workshop manager, not a purchasing agent. Check the panel schedule, the rib spacing, the stripping sequence, and the bolt torque. Ask for the deflection calculation. Then you will know whether the mould will survive 100 cycles or 10.